Alfa Laval Introduces MaxiLobe Rotary Lobe Pumps for Hygienic, High-Purity Processing
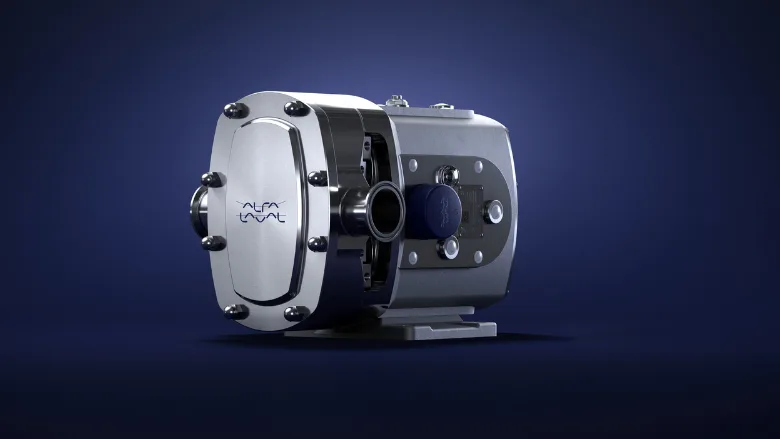
Alfa Laval has introduced its new MaxiLobe and MaxiLobe UltraPure rotary lobe pump ranges, positive displacement pumps designed to improve volumetric efficiency, reduce energy consumption, and simplify maintenance in hygienic and high-purity processing applications.
The pumps are intended for use in dairy, food, and beverage production. According to Alfa Laval, the new ranges offer a broader operating envelope, improved hygienic design, and reduced total cost of ownership compared to previous models.
MaxiLobe pumps are designed to achieve required flow rates at lower operating speeds, potentially allowing manufacturers to use smaller pumps for the same applications. Lower operating speeds can also reduce shear, helping protect shear-sensitive products during processing.
Improved Efficiency and Reduced Operating Costs
According to Alfa Laval, MaxiLobe and MaxiLobe UltraPure pumps offer higher volumetric efficiency and a broader flow and pressure operating range than other models, potentially reducing equipment and installation costs by allowing manufacturers to select smaller pumps for suitable applications.
The company reported that, under defined operating conditions, MaxiLobe pumps deliver at least 5 percent higher flow rates than equivalent Alfa Laval SRU models. Key porting dimensions also match those of all SRU pumps and most SX and SX UltraPure models, allowing manufacturers to replace existing equipment without modifying pipework.
Additionally, Alfa Laval said the pumps can achieve required flow rates at lower operating speeds, potentially delivering energy savings of more than 25 percent in many applications. Lower speeds also reduce shear on sensitive products and mechanical stress on pump components, which may extend service intervals and equipment life.
The pumps also feature a gearbox designed to support reliable performance under demanding operating conditions.
Looking for quick answers on food safety topics?
Try Ask FSM, our new smart AI search tool.
Ask FSM →
Hygienic Design and Regulatory Compliance
MaxiLobe and MaxiLobe UltraPure pumps incorporate precision-profiled elastomers and hygienic design features intended to improve cleanability, protect product quality, and reduce cross-contamination risks.
According to Alfa Laval, the standard MaxiLobe range carries European Hygienic Engineering and Design Group (EHEDG) and 3-A Sanitary Standards certifications and complies with applicable U.S. Food and Drug Administration (FDA) requirements.
Alfa Laval also provides its Q-doc documentation package to support material traceability and validation in regulated manufacturing environments.
Each pump is factory-tested and supplied with a performance certificate confirming that it meets its specified operating curve before delivery.
Simplified Maintenance and Servicing
MaxiLobe and MaxiLobe UltraPure pumps incorporate maintenance features intended to minimize downtime and simplify routine servicing.
Front-loading single seals can be replaced without removing the pump from the process line. Interchangeable components and accessible shimming are also designed to reduce maintenance time.
Alfa Laval said these features, combined with the pumps' lower operating speeds and gearbox design, are intended to improve equipment uptime and reduce lifecycle costs.
Alfa Laval: www.alfalaval.com